Maximizing Production with ASU Industrial Oxygen Plants
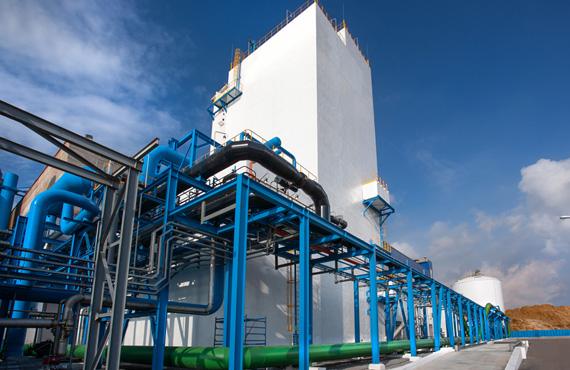
In today’s competitive industrial landscape, maximizing production efficiency is crucial for maintaining a strong market position. One of the key components in achieving this is the utilization of advanced technologies for oxygen production. ASU Industrial Oxygen Plants play a pivotal role in this regard, providing an efficient and reliable source of high-purity oxygen necessary for various industrial processes. This article explores how these state-of-the-art systems can be leveraged to optimize production and enhance operational efficiency.
Understanding ASU Industrial Oxygen Plants
An asu industrial oxygen plant is designed to separate atmospheric air into its primary components ? nitrogen, oxygen, and argon. This is achieved through a process called cryogenic distillation, which involves cooling the air to extremely low temperatures to liquefy it, then selectively distilling the liquid to isolate its components.
Key Benefits of ASU Industrial Oxygen Plants
- High Purity Oxygen Production: These plants are capable of producing oxygen with purity levels exceeding 99%, which is essential for industries such as healthcare, metallurgy, and chemical manufacturing.
- Scalability: ASU plants are scalable to meet varying industrial demands, from small-scale operations to large industrial complexes.
- Energy Efficiency: Modern air separation industrial plants are designed to minimize energy consumption, thus reducing operational costs.
- Reliability and Safety: With advanced control systems, these plants ensure consistent operation and incorporate safety mechanisms to prevent accidents.
Applications in Various Industries
The versatility of air separation industrial units makes them invaluable across a range of industries. Here are some notable applications:
Metal Production
In the steel industry, oxygen is used to enhance combustion efficiency in blast furnaces, improving the quality and reducing the cost of steel production. The integration of industrial api 618 compressors into these systems further optimizes oxygen delivery and pressure management, critical for high-temperature processes.
Chemical Industry
Oxygen is a vital component in the production of chemicals like ethylene oxide and propylene oxide. The high purity oxygen and reliable supply provided by ASU plants ensure consistent output and quality in air separation industrial plant applications.
Healthcare and Environmental Applications
In healthcare, oxygen is indispensable for life support and medical therapies. ASU oxygen plants provide a stable and safe source of medical-grade oxygen crucial for hospital and emergency services. Additionally, oxygen is used in environmental applications such as wastewater treatment, where it aids in the aerobic digestion of organic matter.
Optimizing Production with Advanced Technologies
The deployment of cutting-edge technology in ASU plants is key to maximizing production efficiency. Automation and digitalization play significant roles in enhancing operational effectiveness. Advanced monitoring systems and data analytics allow for:
- Real-Time Monitoring: Continuous monitoring of plant operations ensures adherence to optimal conditions, thus reducing downtime and increasing output.
- Predictive Maintenance: By analyzing operational data, potential issues can be identified and addressed before they lead to equipment failure.
- Energy Management: Intelligent systems help optimize energy use, allowing for adjustments that reduce consumption while maintaining production levels.
Conclusion
Incorporating ASU Industrial Oxygen Plants into production processes offers substantial benefits across various industries. From high-purity oxygen production to energy efficiency and scalability, these plants are integral to achieving enhanced productivity and operational excellence. By embracing advancements in technology and automation, industries can further optimize their processes, ensuring sustainable growth and competitiveness in the global market.
Post Comment